Welcome to
HabPharmaceuticals
LOADING

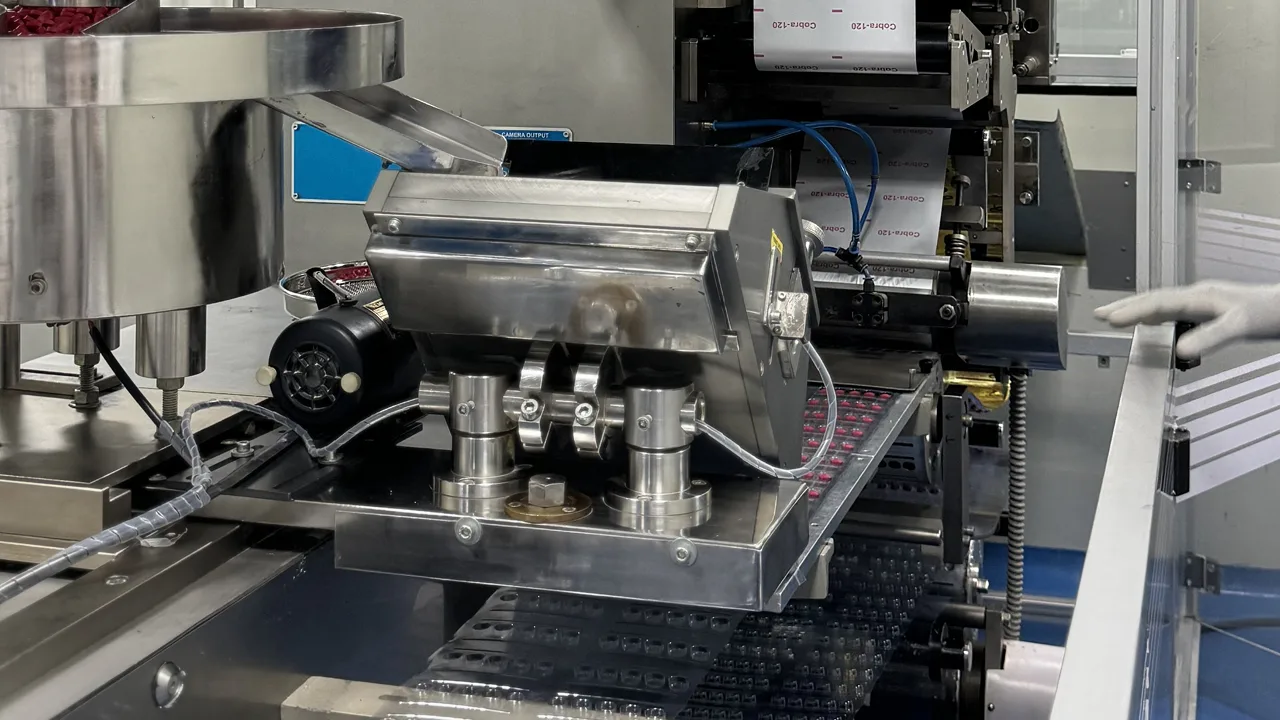

Our facilities are GMP-compliant and regularly audited to ensure every product meets national and international safety standards.

We possess comprehensive capabilities across a wide range of dosage forms, including solid orals, liquids, semi-solids, injectables, and ophthalmics. Our expertise extends to complex formulations such as modified-release and controlled-release systems, designed to enhance therapeutic performance and patient compliance.
Our development process follows a systematic pathway from pre-formulation and compatibility studies to formulation design, analytical method development and stability evaluation. This integrated approach ensures consistency, scalability, and compliance with global quality standards.
We apply Quality by Design principles to build quality into products from the outset. Through risk assessment, design space evaluation, and process optimization, we establish robust and reproducible manufacturing processes that support long-term product reliability.
Our advanced analytical infrastructure supports method development, validation, and stability studies in accordance with regulatory expectations. These capabilities ensure product integrity throughout its shelf life and across varied market conditions.
With a strong focus on scalability, our R&D team enables efficient technology transfer from laboratory to manufacturing. This ensures smooth commercialization, consistent product performance, and readiness for global markets.
Targeted treatments for fast, effective relief from back, joint, and inflammatory pain.

Comprehensive solutions for heart health, blood pressure control, and cholesterol management.

Advanced formulations to support neurological health, sleep disorders, and mental wellness.

Specialized therapies designed to treat acidity, gut health issues, and gastrointestinal conditions.

Precision medicines for metabolic disorders and long-term blood sugar regulation.

Effective care for asthma, nasal congestion, and pulmonary conditions.
Broad-spectrum antibiotics, antifungals, and anti-infectives to combat diverse bacterial and fungal treatments.
Dermatology formulations including serums, creams, and specialized hair care treatments.
Daily essential vitamins, minerals, and dietary supplements to promote overall wellness.
Dedicated healthcare solutions for reproductive health and urological conditions.

Robust solid oral dosage capabilities supporting high-volume production across diverse therapeutic segments.
Specialized topical manufacturing catering to dermatological and external therapeutic applications.
Precision-driven liquid formulations produced under controlled manufacturing conditions.
Established capabilities in sterile injectable manufacturing across key treatment areas.
Advanced dosage formats, reflecting our expertise in complex formulation and specialized delivery systems.

Engineered for high-volume, multi-dosage production, our facilities deliver operational efficiency without compromising on quality.

WHO-GMP and cGMP-aligned systems ensure every product meets rigorous global regulatory and safety standards.

From production to delivery, we maintain reliability across supply chains, supporting partners and patients across international markets.